Swiss Machining: The Technology Behind the World's Smallest Watches
Have you ever wondered how tiny rubies fit perfectly into a watch, how all the thin, small parts and cogs function perfectly without the need for any replacement for a lifetime? And more importantly, why does “Swiss Made” carry such an honor in watchmaking?
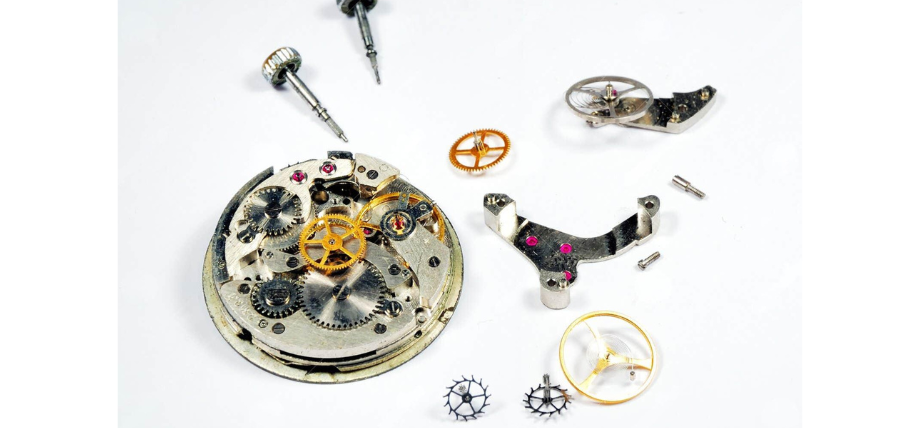
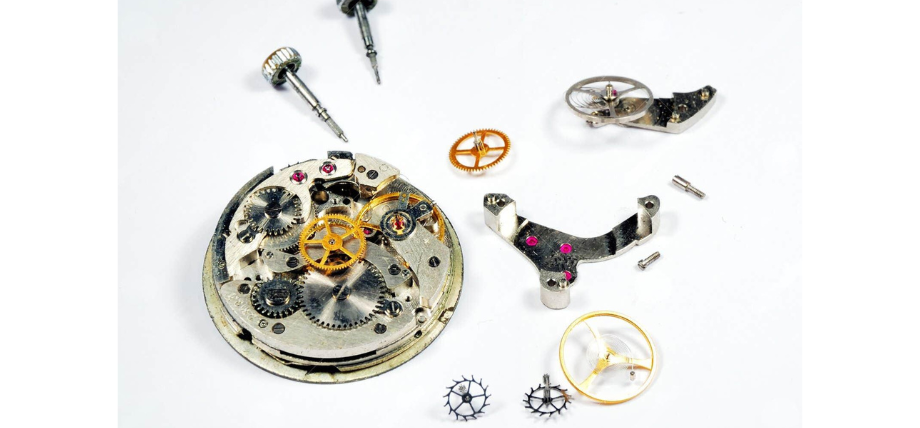
Figure 1: Intricate mechanical watch components.
The answer is Swiss turning or Swiss machining. It is the precision and reliability of CNC machining parts that ensure you are always on time. CNC machining is a subtractive process that "involves removing material from a solid workpiece to achieve complex geometries" [1].
The Machine That Started In Watch Making
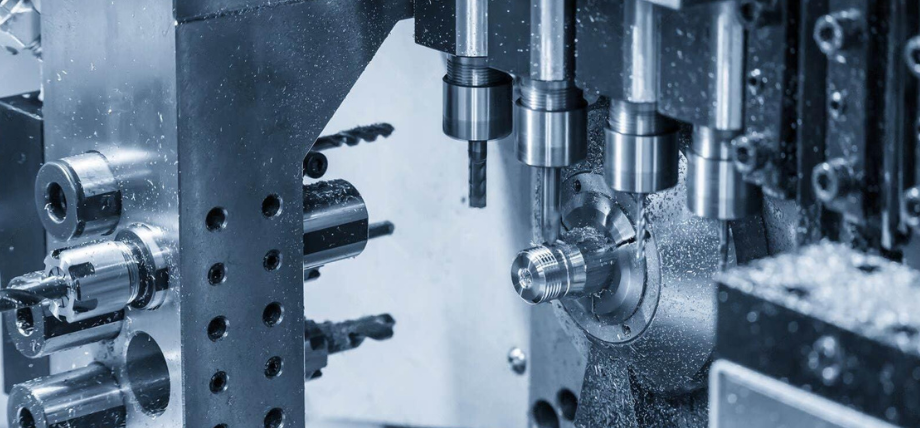
Figure 2: High-precision automated Swiss machining.
During the 1870s in the Jura mountains of Switzerland, a machinist named Jacob Schweizer came across an intriguing physics question. In order to cut a part using a lathe, he would hold one end of a metal bar in his hand while making cuts to the bar as it turns. This created difficulty in terms of leverage. The further away the workpiece was from the part that held the metal, the more the metal flexed away from the tool.
The Schweizer solution was simple and beautiful, and it remains the core of the machine to this day. He employed a guide bushing, which is a steel collar that supports the bar only a millimeter or so away from the cutting point, and allowed the entire headstock assembly to feed the bar through to a stationary tool. Since the metal is supported precisely at the cutting point, the unsupported length becomes essentially zero, and the deflection problem is also addressed. More than a century and a half later, the machine has become computer-controlled, employs live milling cutters, and has an additional spindle, but the basic idea is the same.
Just How Small Can Swiss Machining Go
This machining is small enough that the quantities stop being industrial and become jewelry-like. Swiss lathes will readily machine parts as small as 0.25 mm in diameter and bore holes of a mere 0.10 mm diameter.
The cutting tools employed in machining details will measure less than 0.05 mm in diameter and are therefore smaller than a hair thread. However, this is not done on a single heroic part for a trade show but on thousands, and all identical.
Putting it in perspective
A shaft measuring 0.25 millimeters in diameter is only the same size as two sheets of regular paper placed on top of each other.
A drill hole at 0.10 millimeters is equivalent to just one strand of human hair, which is placed in its correct position in something that is rotating at the very same time. A completed micro-assembly may even be the size of a speck of rice with threads so fine that it takes a magnifying glass to identify them.
What You Can Actually Make at This Scale
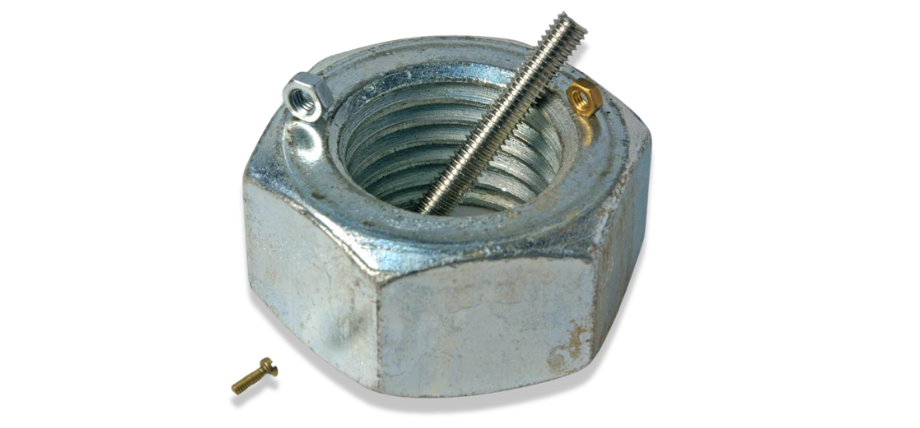
Figure 3: Precision hardware scale comparison.
The significance of Swiss machining for a designer lies in the ability to make something small yet intricate and precise.
Long and impossibly slender
The true value of the guide bushing is the capability to machine parts that have a length substantially greater than their diameter. The metric here is the length-to-diameter ratio; a standard lathe loses control after the ratio reaches 3:1, at which point the part starts whipping around chaotically.
But the Swiss lathe maintains precision with ratios reaching 30:1. Think of machining a one-millimeter diameter shaft and keeping it straight over a thirty-millimeter span.
These kinds of geometries include watch arbors, catheter shafts, and the pins in connectors, all of which require the guide bushing to avoid bending.
Complexity on a miniature body
The Swiss machine is not restricted to the production of only circular components. Along with the feed of the bar, several tool banks act on it sequentially or concurrently – profiling it, cross-drilling holes in its body, creating threads on the surface, knurling the surface for gripping, and milling a flat surface.
The other spindle picks up the component and processes its other surface, followed by the separation of the completed part from the machine. This is termed as "done-in-one," meaning that a finished part comes out of the machine without requiring any further setting up.
Precision That Comes With the Size
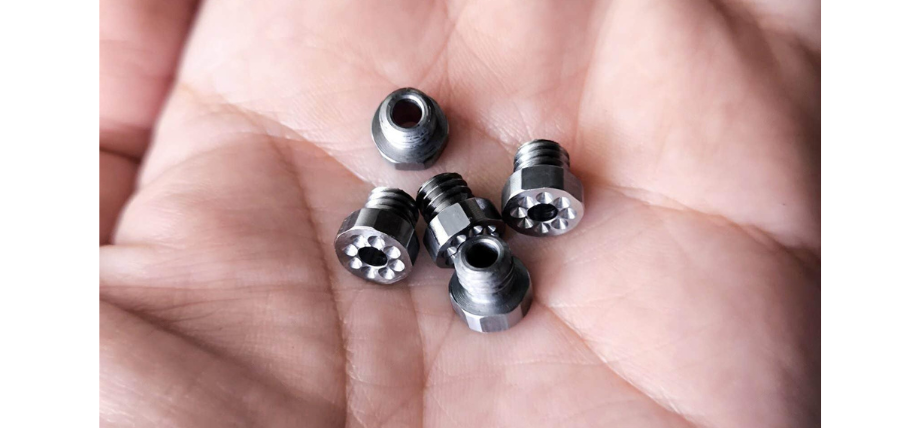
Figure 4: Miniature Swiss machined components.
““Every part not only has to fall within a tight tolerance; it also has to be beautiful.””
What micron tolerances (±0.0025 mm) actually unlock for a designer
Tolerances of Swiss-machined parts range between ±0.0025mm, which is roughly the thickness of one-fortieth of a hair strand. This degree of tolerance affects how your design should be. Components truly become interchangeable: every screw will fit into any thread, and every pin will slide smoothly into any socket without the need for hand-fitting at the bench.
The gears align themselves with a little gap, so watches lose minimal amounts of mechanical energy through friction loss. The press-fit works as a result of the fact that the shaft and bore are matched to within rounding errors. “Advances in precision engineering have driven an increasing demand for systems capable of nanometer-scale resolution and repeatability,” reads Science Direct’s overview on precision machining [2].
Surface finish
In addition to the quality, the same support will also give you the finished product. Parts turned by Swiss precision machines will leave the machines with smooth finishes so much that the need for grinding and polishing is not necessary at all, especially if a buffing wheel cannot even hold the part due to its tiny size.
For watches, however, the requirements are stricter: a pinion or a bridge must impress not only the tolerance gauge but also the naked eye. It is for that reason that watch machinists use the phrase "making artwork" when talking about their craft, since even though the part may measure well, if it is not finished properly, it is a reject. As a designer, this is a privilege you rarely get.
What Materials Are Machinable At This Scale
At that sub-millimeter scale, nearly any metal one might hope for along with some engineering plastics are machinable. Of course, each necessitates different settings and parameters on the machine.
Most metallic materials can be machined easily. Brass is relatively easy to machine and is mostly used for making miniature parts, such as watch parts and joints. 904L Rolex Steel and 316 types of stainless steel are harder to machine than brass; however, they are stronger and more resistant to corrosion and are thus used in surgical equipment and for long-lasting products.
Most may be unfamiliar with Rolex steel which “is a high-alloy austenitic steel distinguished by its elevated nickel and molybdenum content, which gives it superior resistance to pitting and crevice corrosion compared to standard grades like 316L,” which is also used in watch making [3].
Ti-6Al-4V titanium is a particularly useful material that is light in weight, durable, and biocompatible. It is used extensively in making artificial joints, bones, and other medical instruments. Nickel alloys and specialty stainless steels are used in aircraft and medical instruments; gold and platinum are machined into watches and jewelry pieces.
PEEK engineering plastic can also be machined and is used in insulators and some medical parts.
Famous Designs That Are Swiss-Machined
The mechanical watch movement: Small machine parts like pinions, escapement components, and screws are Swiss-machined.
Dental implants and abutments: The titanium screw implant that acts as an anchor for the new artificial tooth and the abutment that connects the implant and crown are Swiss-machined to the smallest tolerances so that infection can be avoided.
Orthopedic bone screws and spinal hardware: Fine screws, rods, and hooks that have to be attached to the spinal column during spinal surgeries are Swiss-machined.
Insulin-pump lead screws: The minute screw that is responsible for advancing the plunger in an insulin pump is basically the dose control unit in itself. The degree of precision of the component translates directly into the dosing accuracy.
The connectors in your electronics: Gold-plated connectors like the contacts, sockets, and spring-loaded "pogo" pins in your phone, laptop, and charger are produced on a massive scale through Swiss turning processes. Every single connection you make with confidence relies on such components.
Conclusion
The connection between a watch, a spinal screw, and the end of the charger's cord is based on one simple principle that goes back 150 years: hold the metal precisely where the cut is made, and the precision makes the small size irrelevant. This is the hidden strength of the knowledge about Swiss machining for any designer.
Through this technology, the horizon of possibility opens up; you can apply a thread, a cross-hole, and a mirror finish on a component the size of a grain of rice and count on receiving it perfectly and identically manufactured. The watch was merely the beginning.
References
[1] "What Is CNC Machining Parts?" PartMfg, www.partmfg.com/what-is-cnc-machining-parts/. Accessed 10 June 2026.
[2] "Precision Machine." ScienceDirect, www.sciencedirect.com/topics/engineering/precision-machine. Accessed 10 June 2026.
[3] "904L Stainless Steel: Watch Making Steel." PartMfg, www.partmfg.com/904l-stainless-steel/. Accessed 10 June 2026.
To cite this article:
Su, Sean. “Swiss Machining: The Technology Behind the World's Smallest Watches.” The BYU Design Review, 10 Jun 2026, https://www.designreview.byu.edu/collections/swiss-machining-the-technology-behind-the-worlds-smallest-watches.